
Thickness and Dimensional Inspection
Every slate dimension lives twice — once on the drawing as a nominal number, once in the stone as a measured one. Inspection is the reconciliation between the two.
The practical standard on the factory floor: thickness read at multiple defined points, length and width measured along defined lines, diagonals compared for squareness — all judged against a tolerance band that was agreed before production, not one invented after the container arrives.
Every Dimension Lives Twice
The caliper reads 24.9. The drawing says 25. Somewhere between those two numbers sits the whole subject of this page.
When billiard slate is bought in quantity, thickness and overall dimensions are not minor details. A set can carry the correct nominal specification on the quotation — 25 mm, 38 mm, 45 mm — and still not measure exactly the same at every point of every piece. Natural slate is a geological material. Cutting, calibration, grinding, temperature, measurement position, and the instrument itself all leave fingerprints on the final reading. The useful purchasing question is therefore not "is the slate exactly 25 mm?" but "how is thickness measured, where is it measured, and what variation is realistic for this type of billiard slate?"
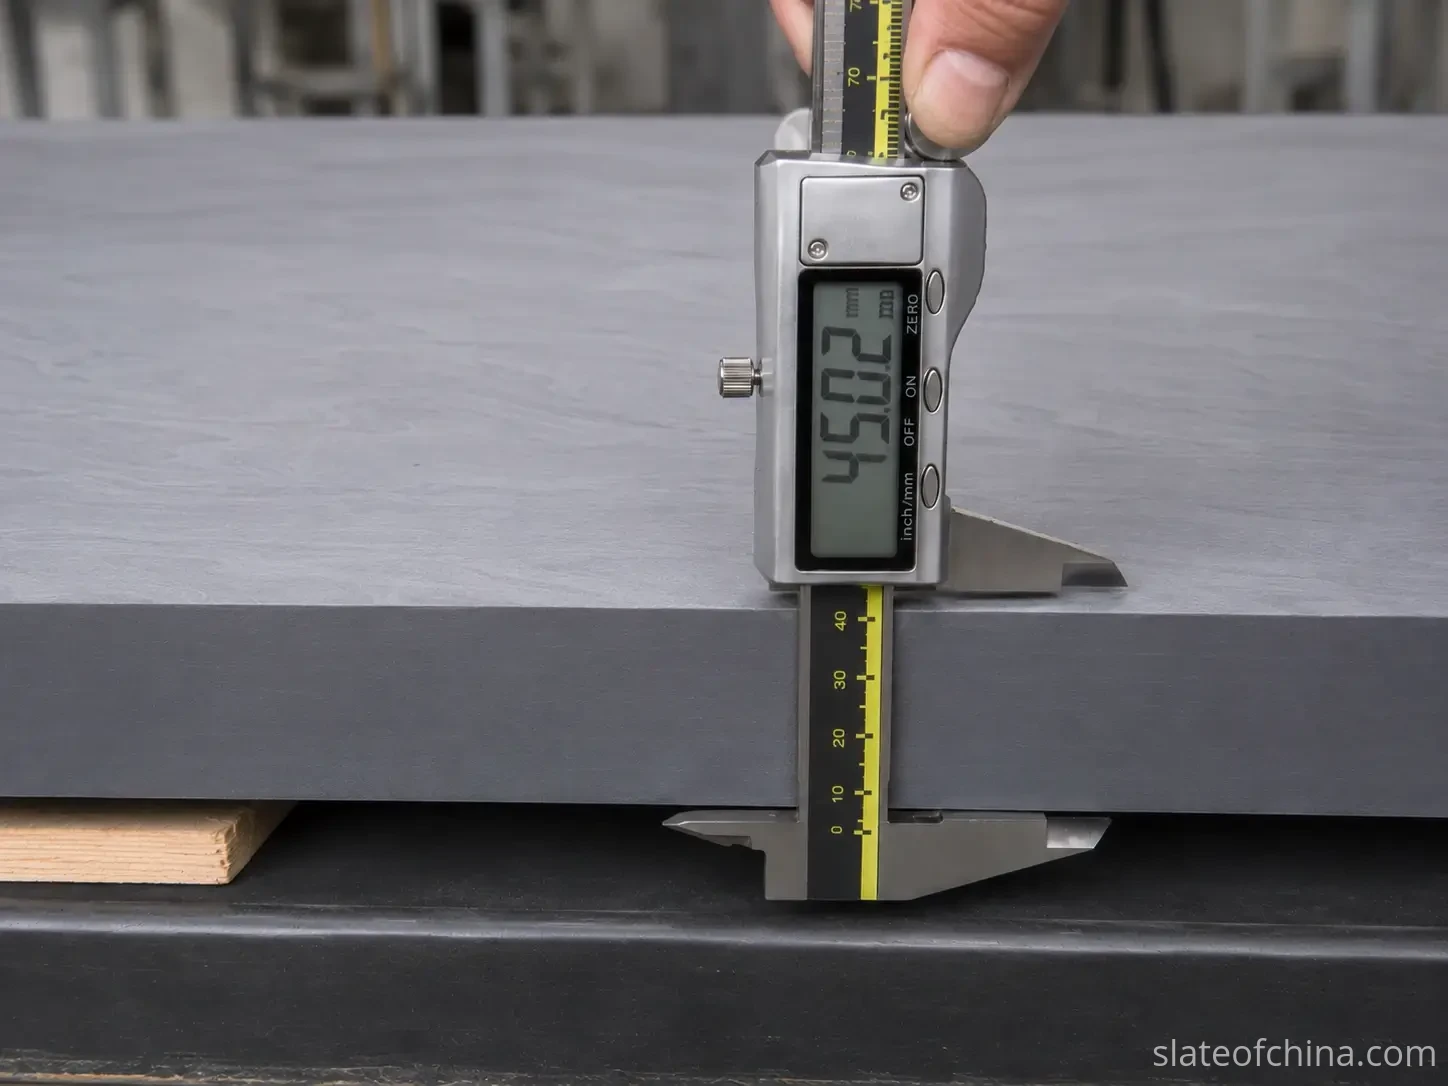
This page explains how we approach thickness and dimensional inspection at the factory, what a workable record looks like, and how to tell normal manufacturing variation from a genuine quality problem. It sits inside a small family of pages, each with its own job: our quality-control guide covers the framework of what buyers check and when; the incoming flatness guide walks the buyer's side of the bench at container arrival; and our quality test data page collects the recorded figures. This one stays on a single lane: thickness and size, and the numbers that describe them.
What "25 mm" Actually Means on a Slate Panel
Billiard slate is ordered to a nominal thickness — commonly 19 or 22 mm for lighter pool tables, 25 mm for the standard 9 ft pool build, 38 to 45 mm for snooker and Chinese 8-ball designs, and 50 mm for heavy-duty frames. The nominal number matters because everything downstream is designed around it: slate weight, frame and support requirements, machining depth, screw and fixing arrangements, shipping weight, and ultimately how the table plays. A 9 ft set at 25 mm typically weighs around 250–270 kg; a 12 ft snooker set at 45 mm across five pieces reaches roughly 800 kg. At a density of about 2.7 t/m³, a millimetre here or there is not a rounding error — it is weight, cost, and structure.
But a nominal size is a target, not a promise written in stone. Suppose an order reads 2718 × 1448 × 25 mm on the drawing. Those three numbers describe what the panels are meant to be. They do not mean that every point on every slate will read 2718.00 × 1448.00 × 25.00 mm — that level of precision is generally unrealistic for a large natural-stone product, and a specification that pretends otherwise is setting both sides up for a dispute.
This is why we treat a claim like "our slate is exactly 25.00 mm everywhere" with suspicion — even when we are the ones being asked to make it. It sounds impressive, but it does not describe how a machined slab actually behaves. A more honest specification defines five things: the nominal dimensions, the measurement method, the measurement locations, the acceptable tolerance, and what constitutes rejection. That turns inspection from an argument into a check. If you are still deciding which thickness to order, our thickness comparison guide covers that choice separately; the technical specifications page collects the standard sizes and weights in one table.
How to Measure Billiard Slate Thickness
Billiard slate thickness should be measured at multiple defined points rather than at a single convenient location. A single reading tells you almost nothing about a large slab. Imagine a 25 mm panel that measures 25.1 mm at one corner. That is one fact about one square centimetre of stone. The same slate could read 24.8 mm at another corner, 25.3 mm near the centre, and 24.9 mm at the opposite edge — and the single convenient reading would have hidden all of it.
So thickness at our factory is checked at multiple defined points, not wherever the gauge happens to land. A practical layout covers the four corners, the midpoints of the four edges, and several locations around the centre. For higher-control OEM orders, additional points are added according to the buyer's inspection plan. On paper the map looks like a grid:
A1 — A2 — A3
B1 — B2 — B3
C1 — C2 — C3
Each letter-number pair gets a real reading, and each reading goes into the record. The purpose is not to calculate one flattering average. It is to see the shape of the variation: consistent thickness, a local thick or thin area, excessive edge variation, uneven calibration, or a systematic production problem. Each of those is a different conversation with the production line.
Where you measure matters as much as how many times. Reading directly over a chipped edge, a rough spot, or a machining transition produces a number that describes the damage, not the panel. That is why the inspection method fixes the location of every point — so the readings describe the slate, not the accidents on its edge.
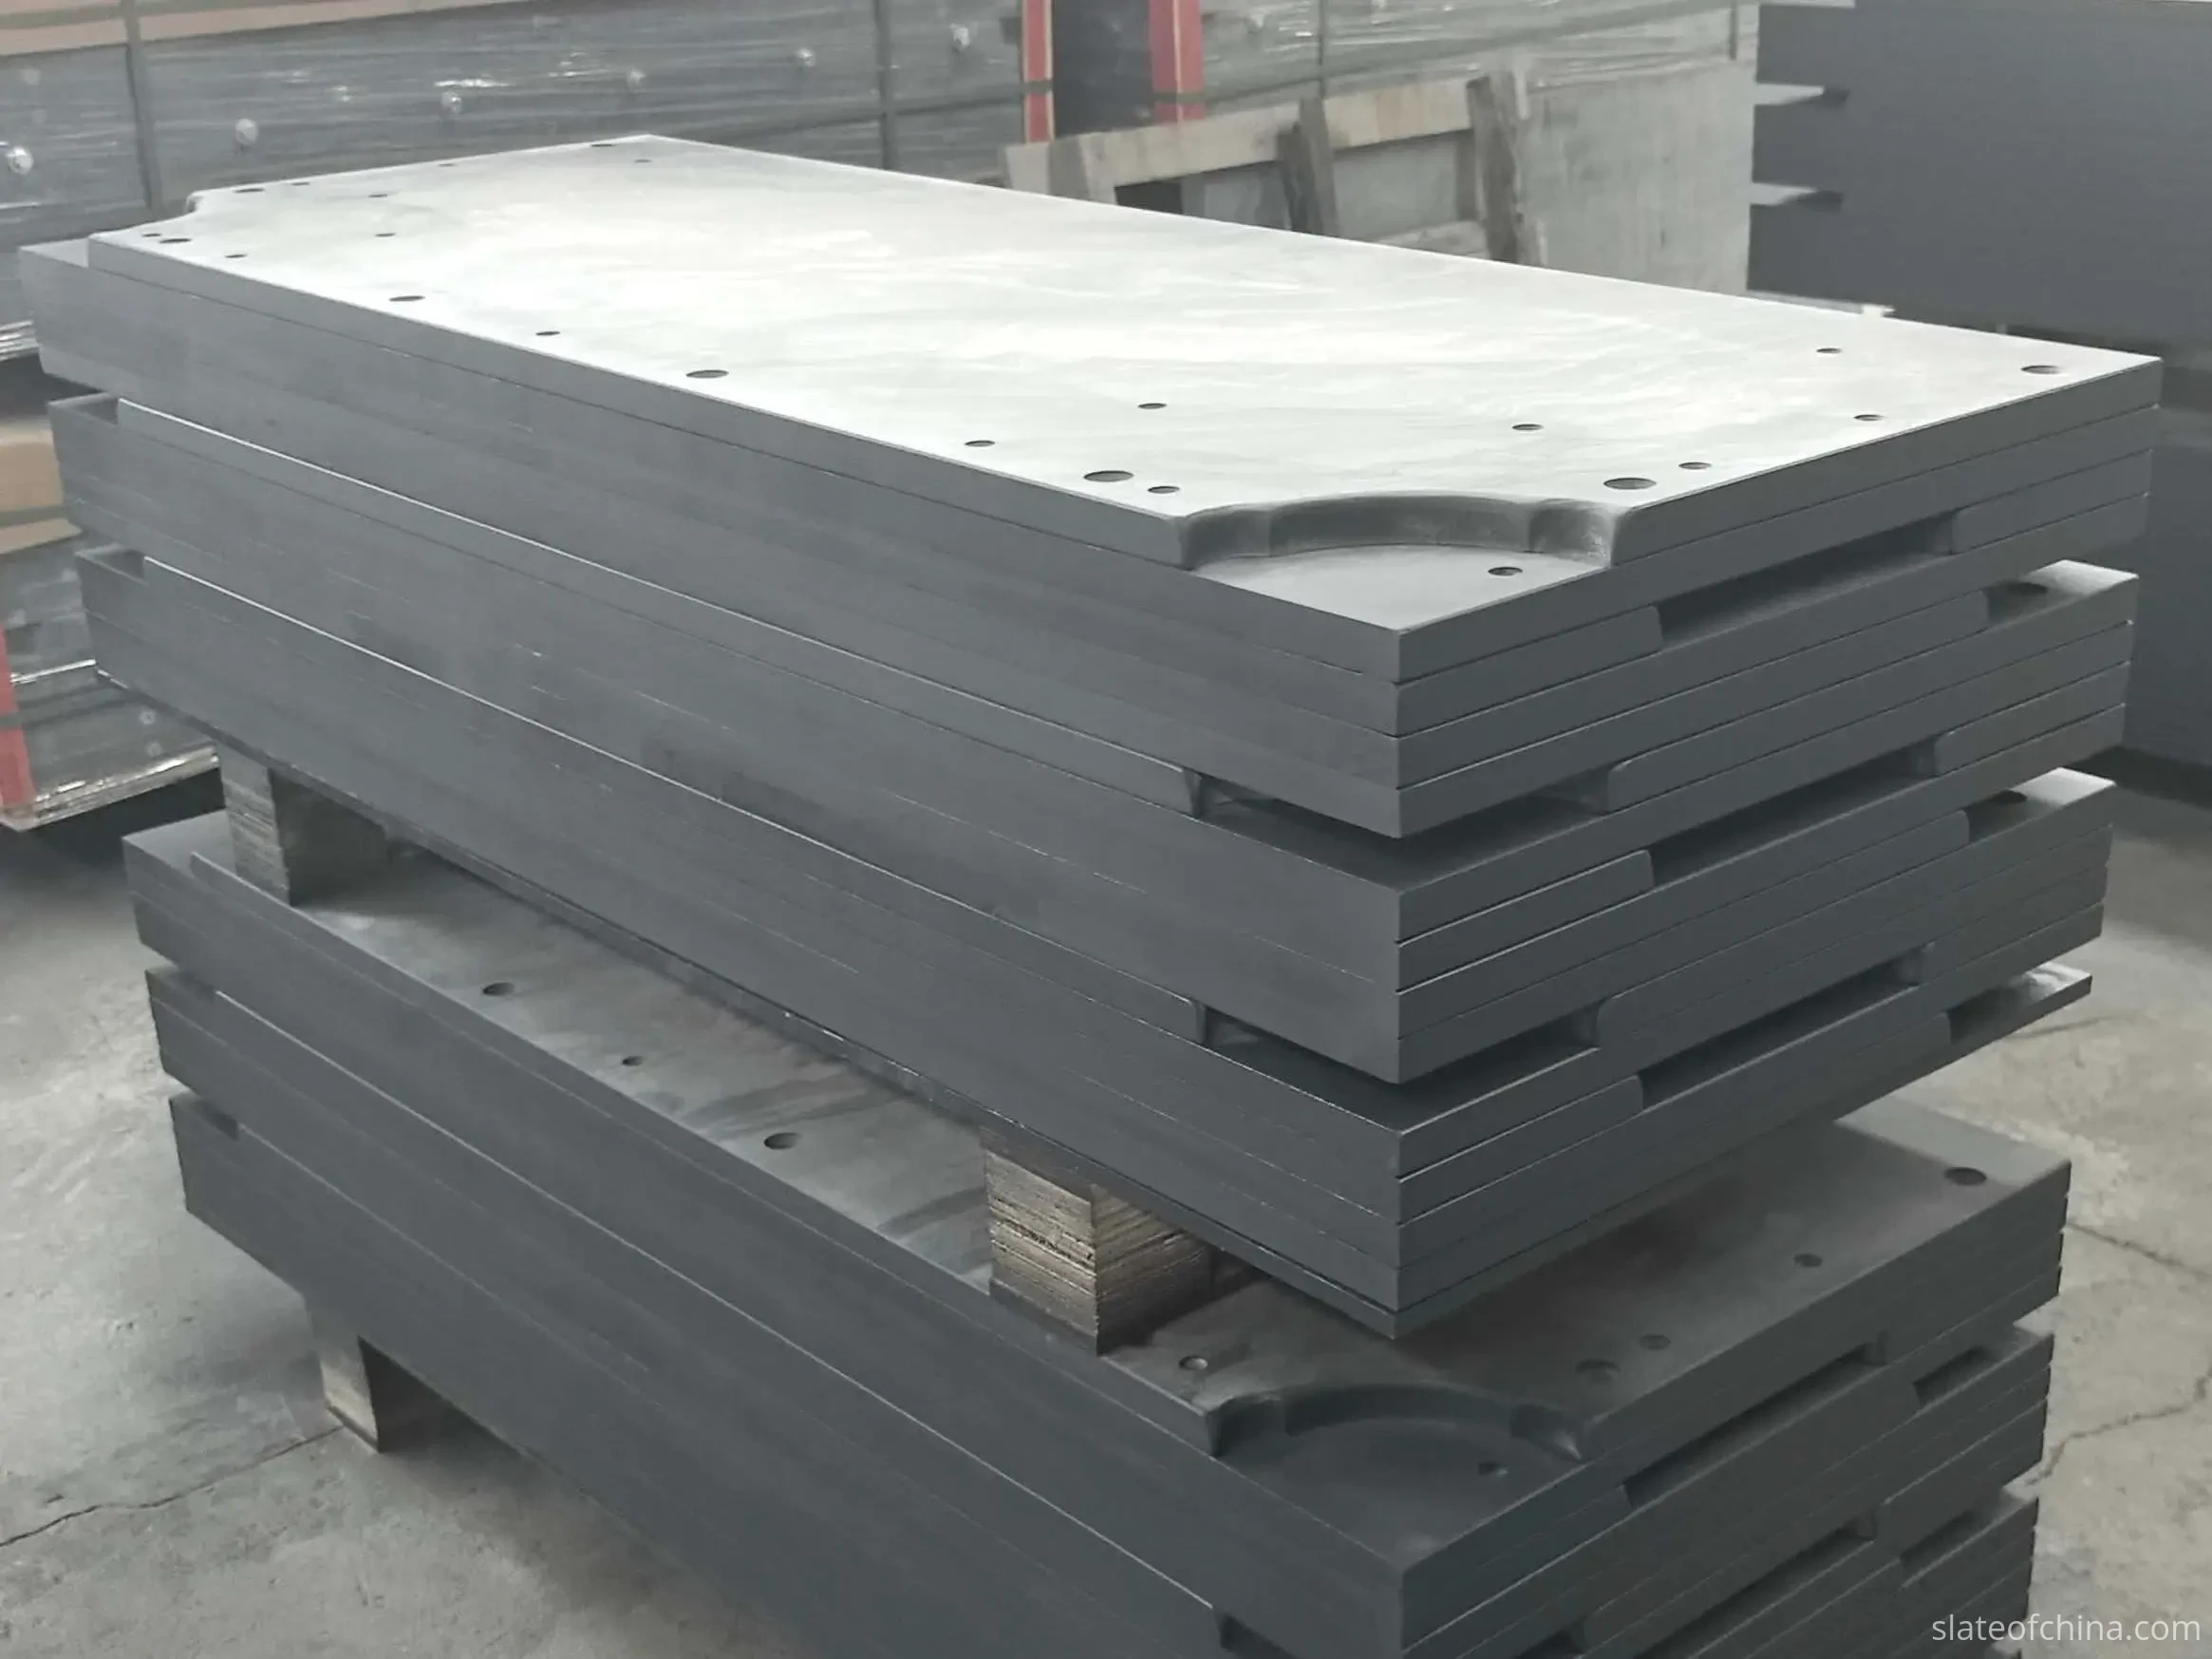
The Tools — and the Trap of Decimal Places
Different instruments suit different jobs, and each has a place where it stops being useful.
| Instrument | What it does well | Where it falls short |
|---|---|---|
| Digital caliper | Fast readings at accessible edges and smaller pieces | Measuring range and consistent positioning become difficult on very large slabs |
| Micrometer | Excellent precision at a controlled, defined point | Not practical for surveying an entire large panel |
| Dedicated thickness gauge | Repeatable readings across large stone surfaces | Only as good as the method behind it — points must still be defined |
| Steel tape / steel rule | Overall length and width | Not suitable for thickness; tape sag affects long-span readings |
Then there is the trap, and it catches experienced buyers too: a display showing 0.01 mm resolution does not mean a large natural-stone slab is manufactured to ±0.01 mm. The instrument's decimal places describe the instrument. The panel's variation describes the panel. What matters is whether the measurement method is repeatable: same points, same instrument, same conditions, same person or a documented handover.
Length, Width, and the Two Diagonals
Overall dimensions follow the same discipline as thickness: measured along defined lines, not judged by eye. For a rectangular panel the record establishes overall length, overall width, thickness at the grid points — and, when squareness matters, the two diagonals.
Diagonals are the quiet heroes of dimensional inspection. Two slates can carry identical length and width and still differ in squareness. The check is simple: measure corner A to corner C, then corner B to corner D. If the two diagonals diverge, the panel carries some degree of out-of-square geometry, edge deviation, or cutting error. For large-format billiard slate this shows up later, during assembly, when a frame expects a rectangle and receives something subtly else. It matters even more for replacement slate, where the panel must fit an existing frame rather than a drawing that can be adjusted to suit it.
On the record itself, a real entry beats a stamp that says OK. An example from a single panel, against a nominal of 2718 × 1448 × 25 mm:
| Measurement | Nominal | Actual |
|---|---|---|
| Length | 2718 mm | 2717.5 mm |
| Width | 1448 mm | 1448.4 mm |
| Thickness — Point 1 | 25 mm | 24.9 mm |
| Thickness — Point 2 | 25 mm | 25.2 mm |
| Thickness — Point 3 | 25 mm | 25.0 mm |
Those are the numbers a buyer can actually work with — they show the size of the deviation, the direction, and whether it lives anywhere that matters. "Passed" tells you none of that.
Supplier A, Supplier B: The Question Behind "25 mm"
Imagine two suppliers, both quoting 25 mm slate. Both send a thickness record. Supplier A reads 25.0, 25.1, 24.9, 25.0, 25.1 mm across five points. Supplier B reads 24.0, 25.8, 24.3, 26.0, 24.7 mm. Both can honestly write "25 mm" on the quotation, because both are quoting the nominal target. But the manufacturing consistency behind the two records is not the same product, and on a table it will not behave like the same product.
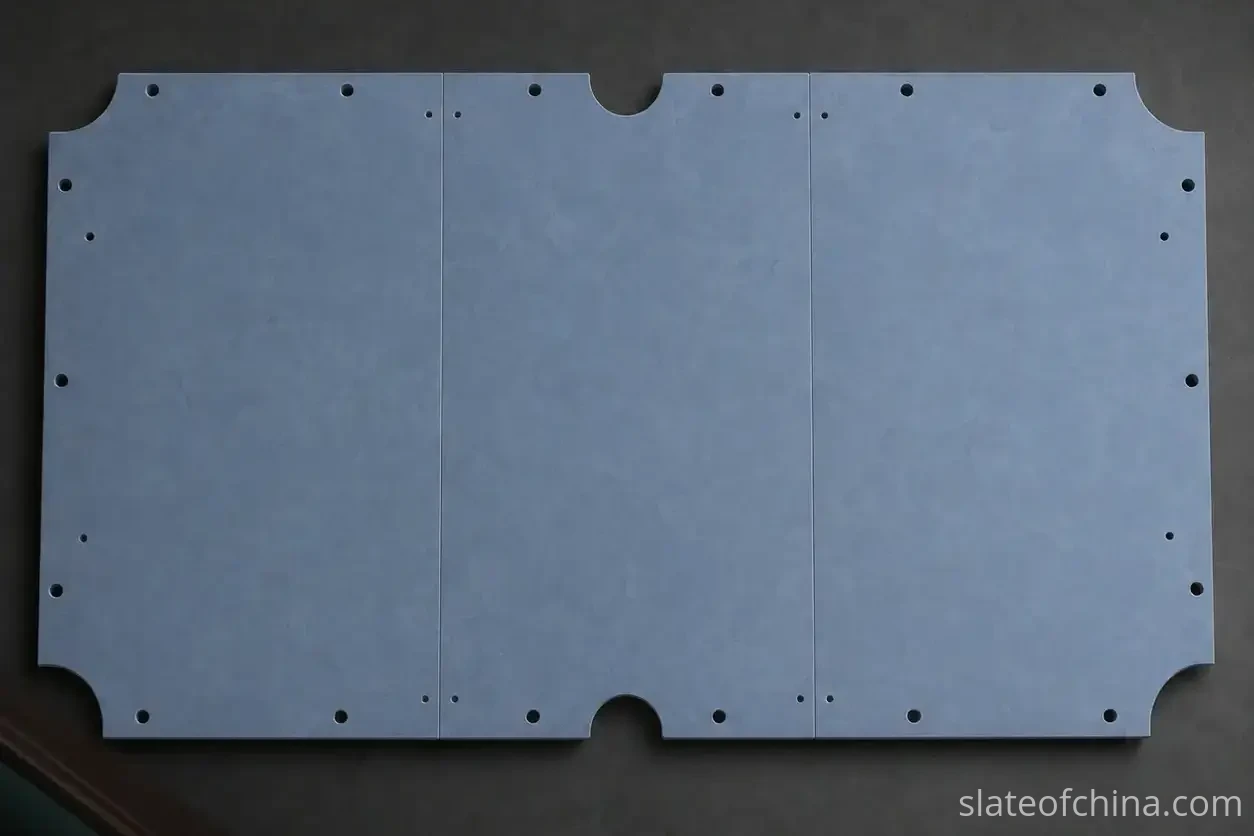
This is why the question professional buyers ask is not "is it 25 mm?" but "what is the maximum thickness variation within one slate?" The first question gets a yes. The second gets a number you can hold the production record against. Small, controlled dimensional variation and large, inconsistent thickness drift are different conditions. The first is how natural stone behaves. The second is a production problem wearing a specification's clothes.
Consistency, in our view, is the actual product. The nominal thickness is just the address where it lives.
What a Realistic Tolerance Looks Like
There is no single universal tolerance that applies to every billiard slate product, and this page will not invent one. A realistic tolerance depends on the nominal thickness, the slate type and size, the calibration and machining process, the measurement method, the table design, and what the downstream assembly actually needs. A tolerance that suits a rough-cut component would strangle a CNC-machined OEM panel; a tolerance written for a tournament table may be wasted money on a home build.
What we can say directionally is this: on machined billiard slate, the thickness conversation normally happens in tenths of a millimetre, not whole millimetres — but the specific band belongs in your purchase specification, matched to your measurement method, not in a supplier's brochure. The format that works looks like this:
Nominal dimensions: ___ × ___ × ___ mm
Agreed thickness tolerance: ± ___ mm, measured with a ___ at the defined grid points
Agreed length/width tolerance: ± ___ mm, measured along defined edges
Squareness: two diagonals compared, difference within ___ mm
Sampling: ___ pieces per production batch, inspection scope agreed per order — full or sampling
Two cautions when filling in the blanks. First, do not select a tolerance because it looks small on paper — select one that matches the table-building process, because the frame, the joint system, and the cloth have to absorb whatever the tolerance allows. Second, do not copy a tolerance from another supplier without checking whether the measurement method and reference conditions are comparable. Two factories writing the same number may be measuring two different things.
And the timing rule that prevents most disputes: the tolerance is agreed before production, not negotiated after delivery. A specification that arrives after the container does is not a specification — it is an opening position. For the recorded figures behind our own production, see our quality test data; for the broader supplier evaluation, our manufacturer selection guide lists the questions that separate a process from a promise.
Five-Piece Sets: The Set Is the Unit
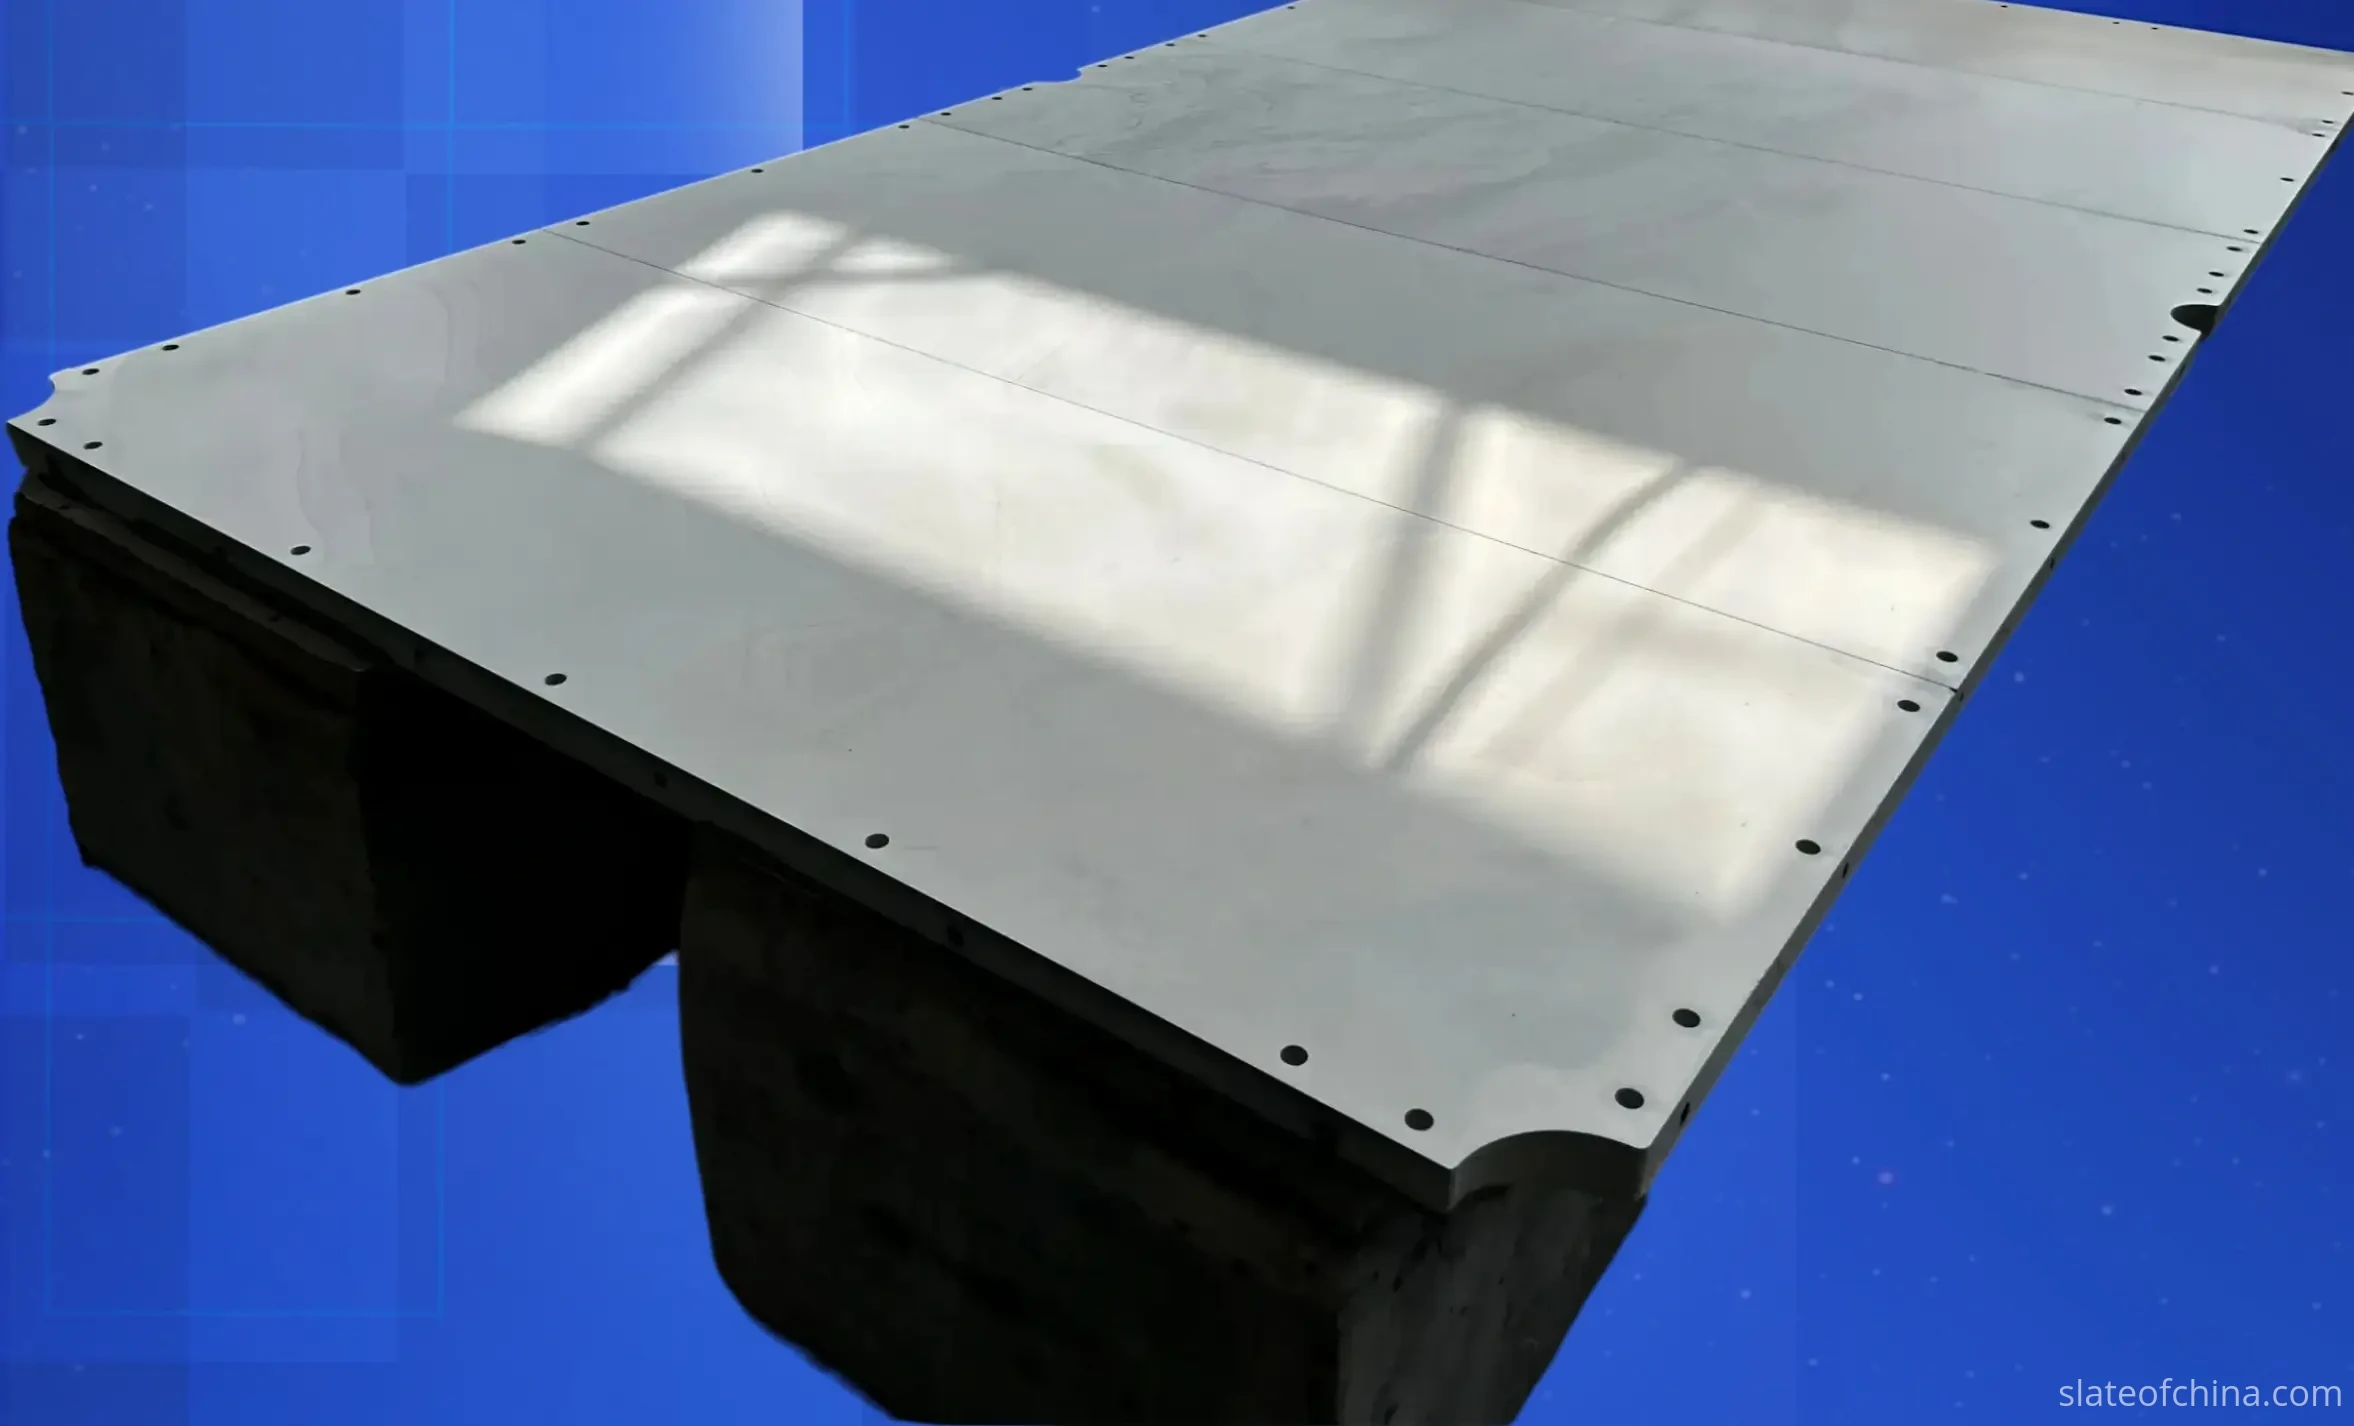
For a five-piece snooker set — or any three-, four-, or five-piece configuration — the inspection does not stop at individual panels. The set is the unit the customer installs, and the relationships between the pieces carry as much weight as any single reading. Per set, the record covers the length and width of each piece, thickness at multiple points, diagonals where applicable, machining dimensions, joint locations, and the identification number of every panel.
The identification system is the part buyers underestimate. A simple scheme — SOC-01-1 through SOC-01-5, one number per panel, marked on the stone and repeated on the record — turns a vague complaint into a workable investigation. "One piece is too thick" is not a report; no factory can act on it. "SOC-01-4, Point B2: 25.7 mm" is a report: production can pull the original record for that panel, check the machining batch, the operator, the instrument, and the day's other results, and tell you what happened. Traceability is not bureaucracy — it is the difference between a quality conversation and an argument.
How many pieces a set should have in the first place — one, three, or five — is a separate decision, covered in our manufacturers' piece-count guide.
Why Thickness Matching Between Panels Matters
For a multi-piece billiard slate set, the important question is not whether every panel has exactly the same average thickness. What matters is whether adjacent panels meet at the joints without a significant height difference. Two panels can each sit close to the nominal and still misbehave at the seam:
Panel A average 25.0 mm, Panel B average 25.1 mm — the averages are close; nothing here signals a problem.
Panel A joint edge 25.0 mm, Panel B joint edge 25.5 mm — a half-millimetre step at the seam.
The averages are nearly identical; the mating edges are not. The joint is where the ball crosses and where the cloth has to bridge whatever the panels leave behind — which is why the record keeps thickness at the mating edges as its own entry, not as a footnote to the panel average. How those joints are machined and verified so the surface stays continuous is the next page in this section: slate joint alignment.
Factory Numbers vs Container-Arrival Numbers
Here is a quiet truth of international slate trade: the factory measures one thing, the buyer's warehouse measures a close cousin of it. We read thickness immediately after machining, in our hall, on our instruments, at our grid points. Weeks later the buyer reads the same panels after ocean transport, unloading, and a different room's temperature, possibly with a different instrument, possibly at different points, possibly by a different hand. Small differences between the two records are not just possible — they are normal, and they do not automatically mean either side is wrong.
When the numbers disagree, the first move is not blame — it is comparison. Line up six things before anyone picks up the phone in anger: the measuring instrument, the measurement location, the measurement method, the environmental conditions, the zero and calibration status of both tools, and the timing of each reading. Most "the factory lied" disputes dissolve at step two, when it turns out the buyer measured a rough edge at a point the factory never used, or compared a single-edge reading against a five-point record.
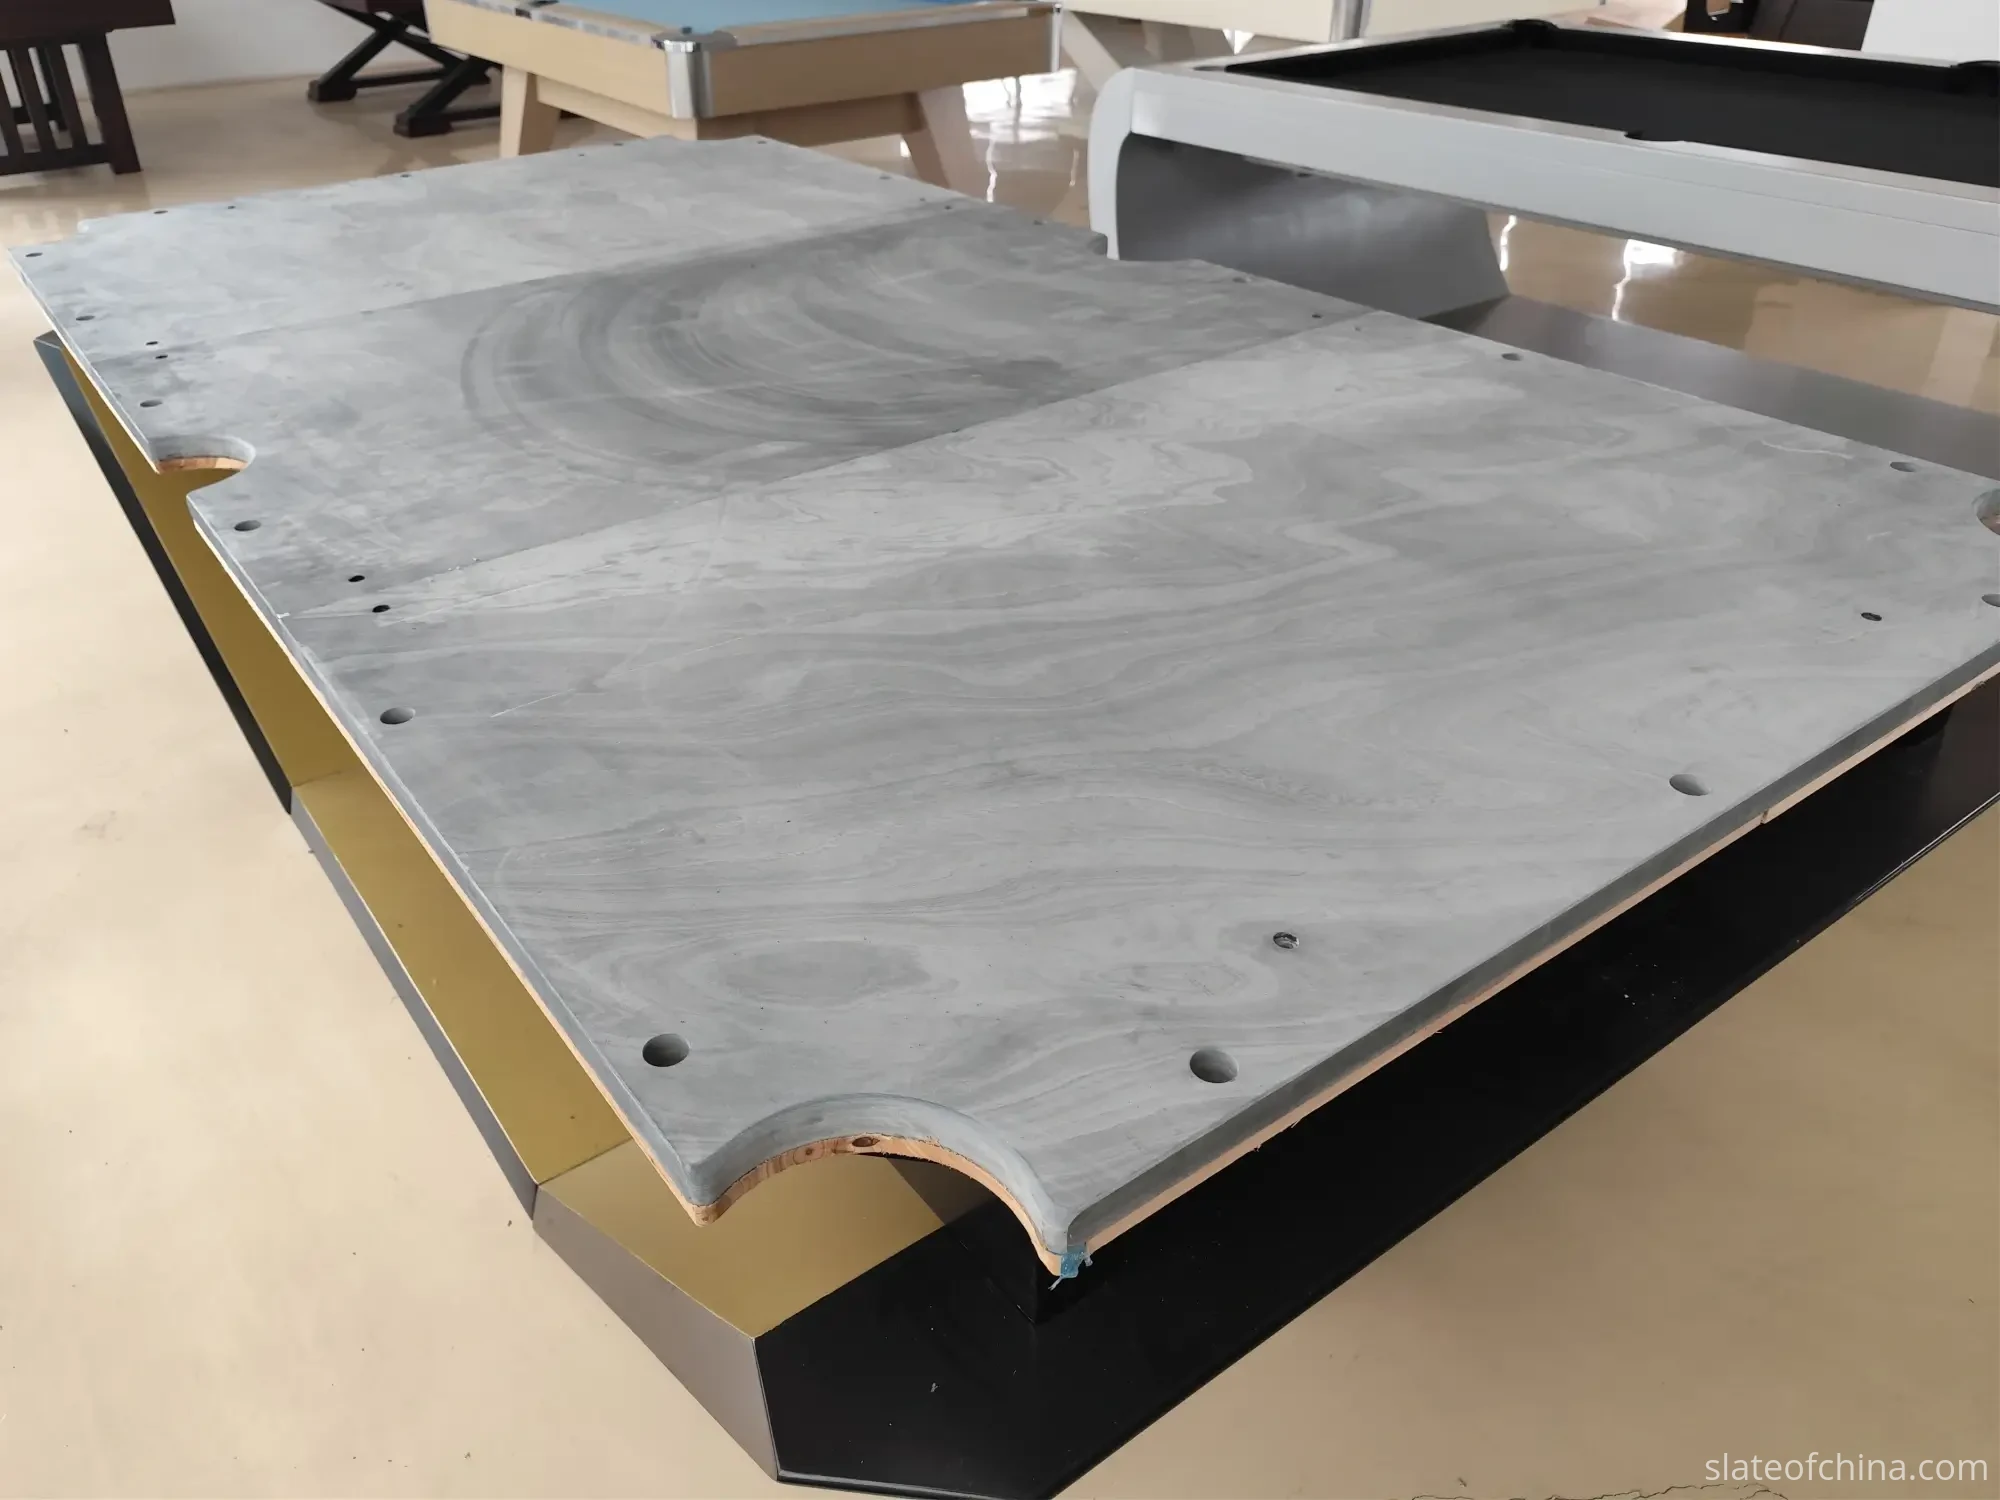
In practice, the bigger causes of mismatched numbers are rarely exotic. Different measurement points. Different instruments. Poor instrument positioning. Reading a chipped edge. Too few points on a large panel. In other words, measurement procedure matters more than chasing decimal places — which is exactly why a clearly written inspection procedure, agreed by both sides, is one of the cheapest quality instruments in international B2B trade. The buyer-side half of that procedure — how to re-check flatness and dimensions when the container arrives — is laid out in our incoming inspection guide.
The Report That Actually Helps
A useful inspection report shows data, not adjectives. It does not need to be beautiful; it needs to be specific. A workable format:
| Item | Specification | Actual result | Status |
|---|---|---|---|
| Length | 2718 mm | 2717.6 mm | Pass |
| Width | 1448 mm | 1448.3 mm | Pass |
| Thickness P1 | 25 mm | 25.0 mm | Pass |
| Thickness P2 | 25 mm | 25.2 mm | Pass |
| Thickness P3 | 25 mm | 24.9 mm | Pass |
| Thickness P4 | 25 mm | 25.1 mm | Pass |
| Diagonal A–C | Agreed | Recorded | Pass |
| Diagonal B–D | Agreed | Recorded | Pass |
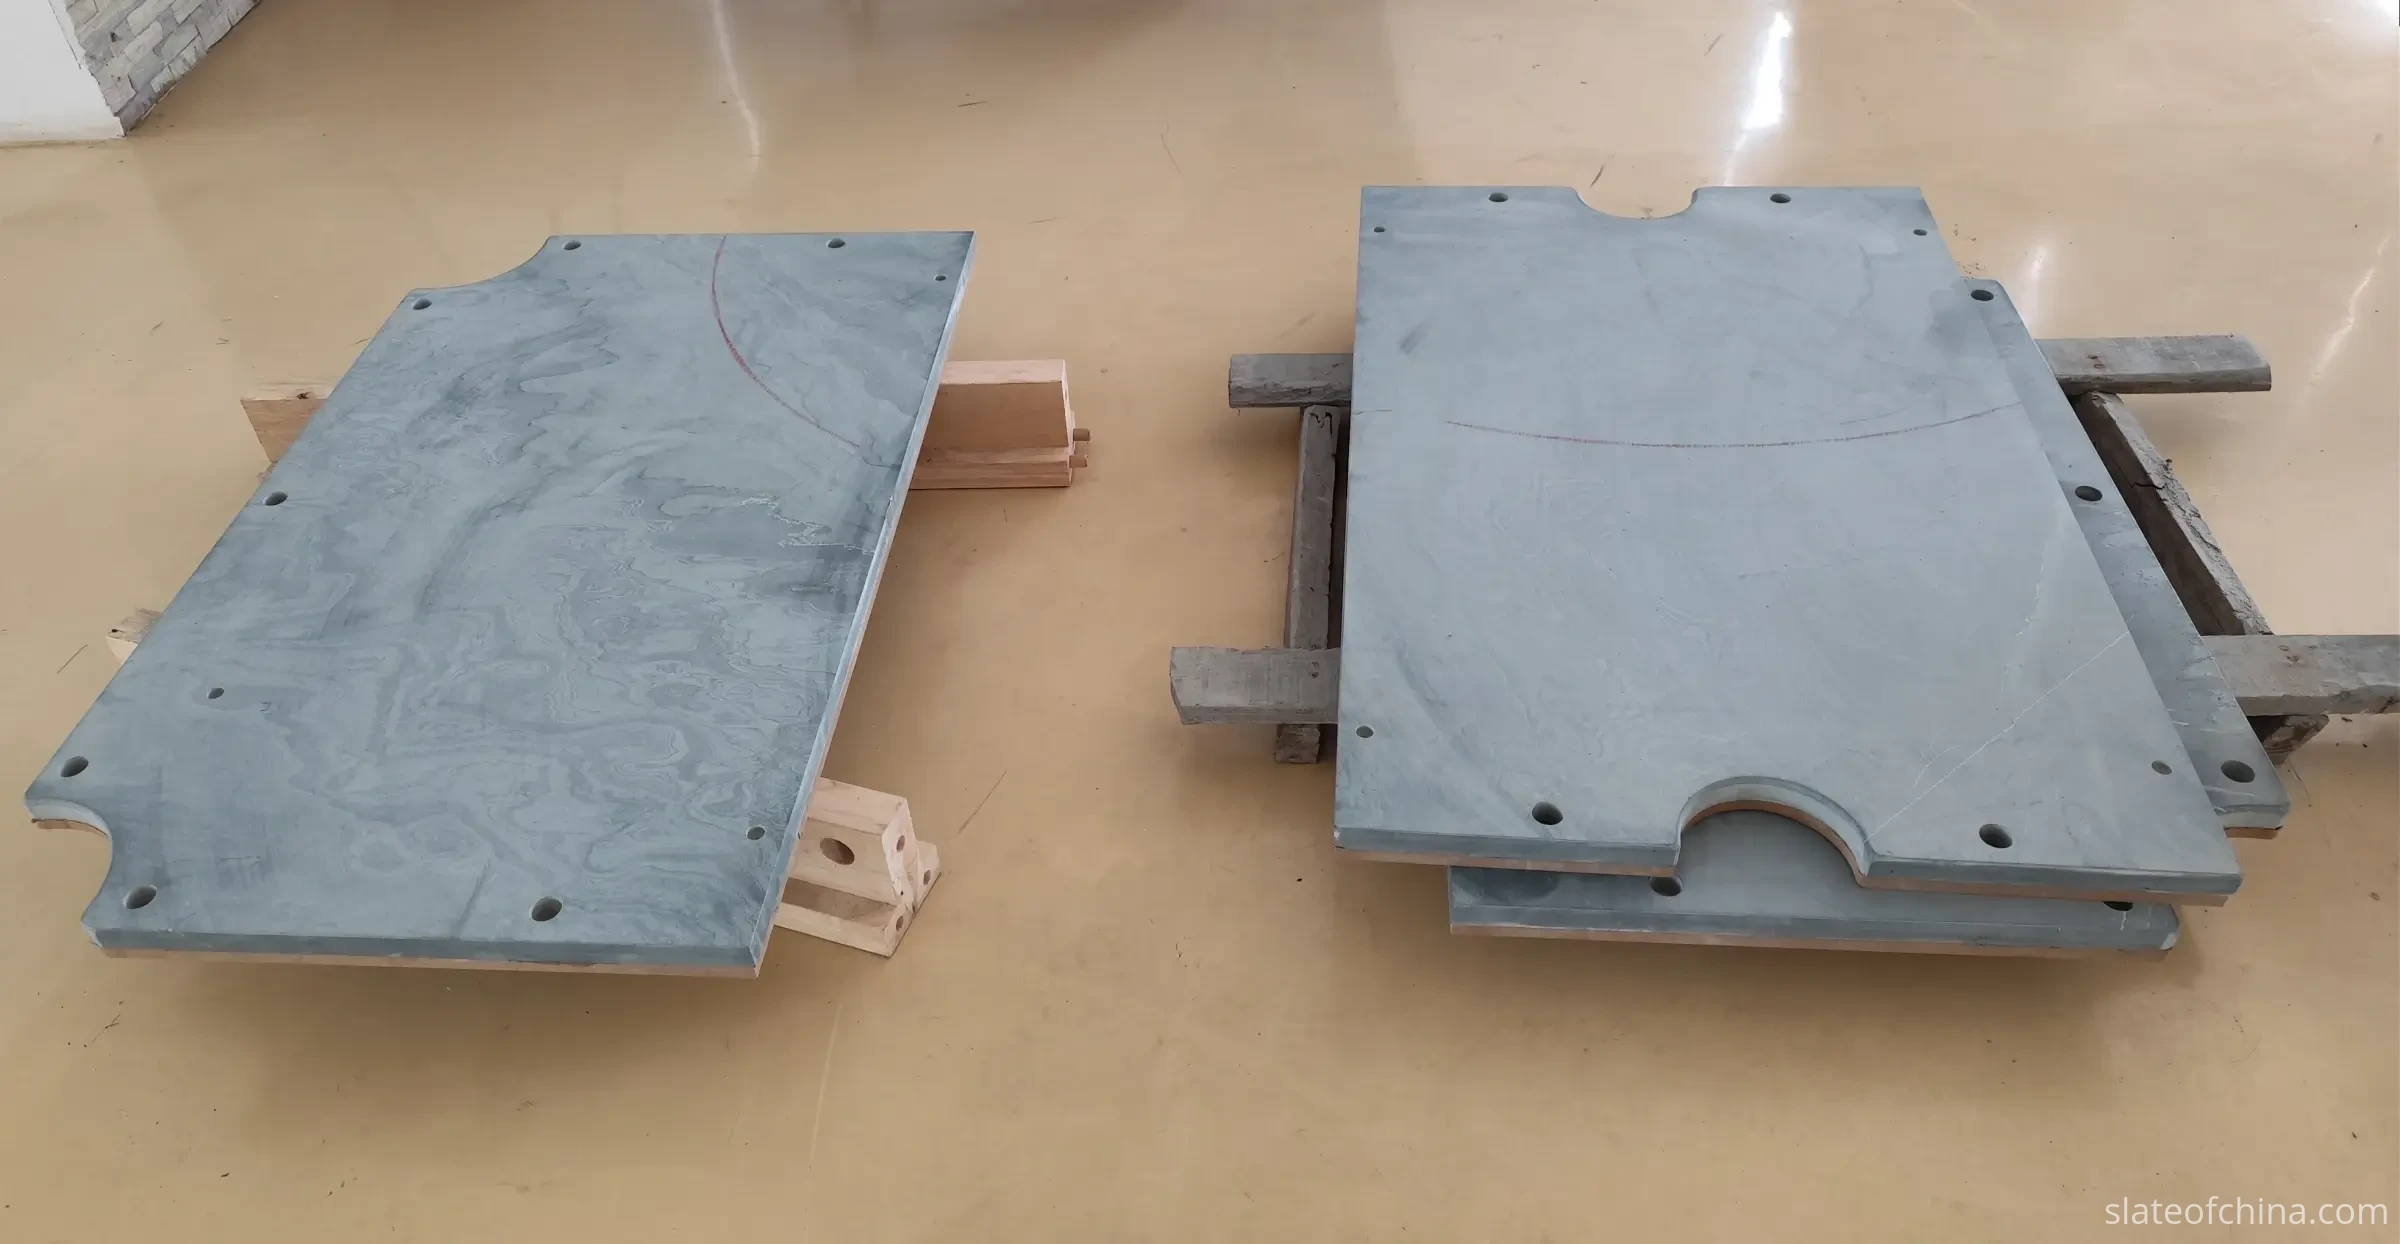
The acceptance limits behind each "Pass" come from the agreed purchase specification — never from a generic standard, and never from memory. The principle behind the whole document is a sequence: measure → record → compare → decide. The alternative — look, judge, pass — is not inspection; it is an opinion with a signature. When a reading falls outside the band, photograph the measuring setup with the reading visible, note the piece number and the point, and let the record carry the argument.
What to Settle Before the First Panel Is Cut
Everything above becomes easier when it is arranged before production rather than argued after arrival. Before a large order is placed, buyer and factory should have the same answers to a short list: nominal length, width, thickness and pieces per set; the thickness tolerance and the length/width tolerance; the squareness requirement if the design needs one; the measurement method — which instrument, which points, how many; the sampling plan — how many pieces per batch, and whether inspection scope is full or sampling; and what documentation the buyer receives: inspection records, measurement photos, production photos, piece identification, and the pre-shipment report.
When a buyer asks us, "can you guarantee exact dimensions?" — the honest answer is that the question is aimed at the wrong target. The workable version is: "what dimensional tolerance can you consistently maintain, and how do you measure it?" A supplier worth ordering from can explain how the slate is cut, how it is calibrated, where thickness is read, how variation is controlled, and how the final inspection is recorded. That explanation is much stronger evidence of capability than a promise of perfect size — and much easier to verify against the report that follows the container.
Frequently Asked Questions
What is a realistic thickness tolerance for billiard slate?
There is no single number that applies to every table, size, and manufacturer — the tolerance depends on the nominal thickness, the machining process, the measurement method, and what the table design needs. On machined billiard slate, tolerance discussions normally happen in tenths of a millimetre rather than whole millimetres, but the specific band belongs in your purchase specification, agreed before production. Any supplier quoting a universal tolerance without stating the measurement method and reference conditions is not describing a measurable standard.
How many points should I measure for slate thickness?
A single reading cannot represent a large slab. A practical layout covers the four corners, the midpoints of the four edges, and several points around the centre — nine positions on a simple grid. For higher-control OEM orders, additional points can be added according to the buyer's inspection plan. The goal is not an average; it is to see the shape of the variation and catch local thick or thin areas that one convenient reading would miss.
Why does my measurement differ from the factory report?
Because the two readings were taken in different worlds: different instruments, different measurement points, different environmental conditions, possibly weeks apart and after ocean transport. Before treating the difference as a quality problem, compare the instrument, the location, the method, the temperature conditions, the zero and calibration status of both tools, and the timing. Most discrepancies resolve at the method-comparison stage rather than at the slate.
Does slate thickness affect table weight and shipping cost?
Yes, directly. At a density of about 2.7 t/m³, thickness is the main driver of slate weight. A 9 ft pool set at 25 mm typically weighs around 250–270 kg; a 12 ft snooker set at 45 mm across five pieces reaches roughly 800 kg. Thickness changes the shipping weight, the container plan, and the frame and support requirements — which is why the nominal thickness should be settled with the table design, not improvised at the quotation stage.
How do I check that a slate panel is square?
Compare the two diagonals. Measure corner A to corner C, then corner B to corner D. On a true rectangle the two diagonals match; a meaningful difference between them indicates out-of-square geometry, edge deviation, or cutting error. Length and width alone cannot reveal this — two panels with identical length and width can still differ in squareness, which matters at assembly time and matters even more for replacement slate that must fit an existing frame.
Should every piece in a multi-piece set have exactly the same thickness?
What matters is that adjacent panels match at the joints — thickness at the mating edges, alignment of the joint surfaces, and a height difference small enough to disappear under the cloth. The pieces are machined as a set, and the record is kept per piece with identification numbers, so any single panel can be traced back to its own readings. Demanding exactly equal numbers at every point of every piece is not how a natural-stone product behaves; demanding a matched, documented set is entirely reasonable.
Quick Reference: Thickness and Dimensional Inspection
| Inspection item | How it is checked |
|---|---|
| Nominal thickness | Grid of defined points — corners, edge midpoints, centre — never one convenient spot |
| Thickness variation | Spread across all points; the record shows the maximum, not just an average |
| Length and width | Measured along defined lines against the drawing, not judged visually |
| Squareness | Two diagonals compared; a meaningful difference signals out-of-square geometry |
| Set matching | Adjacent panels compared at joints — thickness, alignment, height difference |
| Identification | Every panel numbered (e.g. SOC-01-1 to -5) and tied to its own readings |
| Sampling | Inspection scope agreed per order — full or sampling, defined before production |
| Documentation | Measured values + photos + piece IDs + method + reference conditions |
| Acceptance | Compared against the agreed tolerance band — never a generic standard |
A nominal size is a target. A documented measurement is a fact. Reconciling the two, before the container leaves, is what dimensional control actually means.
Related Reading
Sending a drawing? Ask for the measurement plan that comes with it.
Tell us your table type, nominal dimensions, thickness, piece count, and how tight your assembly needs the tolerances to be. We will confirm the measurement points, method, and sampling plan before the first panel is cut — so the numbers on the report match the numbers on your drawing.